About Farleygreene
We are a family-owned business committed to bringing you the most efficient sieving solutions on the market.
In 1976 our founders Peter Davies and Alan Hare saw an unmet demand from manufacturers across a variety of industries who wanted higher quality, bespoke sieving solutions.
Decades of developing sieving machinery to meet customer requirements led us to design more effective standard models that maintain the flexibility of individual requirements. This expertise has enabled us to provide equipment to some of the world’s largest food and beverage, pharmaceutical, chemical, and additive manufacturing companies.
A commitment to continuously improve and develop our products and service made it possible for us to create some of the most efficient sieving systems on the market, attracting a network of trusted agents who distribute equipment to customers worldwide.
Today, Farleygreene is owned by one of the founder’s sons, Managing Director: Antony Hare who leads a team of technical and proactive thinkers. Machinery is designed to an exceptional standard using the latest SolidWorks Computer-Aided Design packages and assembled in our Hampshire-based factory using parts manufactured in the United Kingdom.
We consistently meet high standards of quality across our product range and have been awarded an ISO 9001 certification to demonstrate our commitment.

Why Farleygreene?

At Farleygreene we are part of the Made in Britain campaign community that promotes UK manufacturing.
Using the latest SolidWorks CAD software, our engineers design all machinery to an exceptional standard using parts manufactured in the UK. Our production team assemble all our equipment on site at our Hampshire based factory before it’s shipped worldwide.
The Made in Britain objective is to unite, support and promote British manufacturers who produce British products. We work closely with our local supply chain, monitoring every part of the process from beginning to end. This is the only way we can maintain quality with the flexibility that our customers expect. As a company who are proud to produce high quality British made goods, we feel it’s important to maintain this label and make our customers aware of this.
Keep an eye out for the official marque displayed on our products and marketing materials.
How we Approach Customer Projects
We deliver a consultative approach to our sales process from initial request all the way through to after sales support. We take the time to understand your requirements and work with you to find the best, most effective product.
As a company we follow the ISO 9001 Quality Management System to ensure customer satisfaction throughout the duration of each project, whilst striving for continuous improvement of our products and services.
Our Sales Process
We take you through our six-step sales process to ensure that finding the correctly specified equipment is straightforward and the lifespan of the project goes as smoothly as possible.
-
Tell Us About Your Project
Please get in contact with us either by telephone +44(0) 1256 474 547, email [email protected], send us a message via our website form, or find your local Farleygreene distributor to discuss your project requirements.
-
What Can We Do for You
We will respond to you within 2 working days to discuss how we can help you with your project and send you some further information relevant to your application.
-
From Expectations to Solutions
We gather all the data/knowledge you have about your requirements, the environment surrounding the process. With this we will work to put together a quote that answers all your requirements.
-
Getting It Right
Free documented internal testing or free two week machine hire, is available to help you make your mind up. If you’re ready to place an order with us we will ask you to fill in a couple of documents and agree on a timeline for your project.
-
Working Together
An order confirmation will be sent to you, followed by an approval drawing for you to sign off. Once delivery of your order is organised, we will provide you with a tracking number so that you can plan the logistics on the day.
-
Supporting You Along the Way
We will support you as best as we can through the completion of your project and beyond through our after sales service and Spare Parts department.
Tell Us About Your Project
Please get in contact with us either by telephone +44(0) 1256 474 547, email [email protected], send us a message via our website form, or find your local Farleygreene distributor to discuss your project requirements.
What Can We Do for You
We will respond to you within 2 working days to discuss how we can help you with your project and send you some further information relevant to your application.
From Expectations to Solutions
We gather all the data/knowledge you have about your requirements, the environment surrounding the process. With this we will work to put together a quote that answers all your requirements.
Getting It Right
Free documented internal testing or free two week machine hire, is available to help you make your mind up. If you’re ready to place an order with us we will ask you to fill in a couple of documents and agree on a timeline for your project.
Working Together
An order confirmation will be sent to you, followed by an approval drawing for you to sign off. Once delivery of your order is organised, we will provide you with a tracking number so that you can plan the logistics on the day.
Supporting You Along the Way
We will support you as best as we can through the completion of your project and beyond through our after sales service and Spare Parts department.
We Provide You with Certified Products
We understand there are standards you must meet. That’s why we provide full certification of all equipment, to comply with audit procedures, as well as design, installation and operation qualifications where required.
Our commitment to strict working practices has earned us our ISO 9001 Certification, guaranteeing a high level of quality throughout the build of your machine.
All machines conform to CE, UKCA, FDA and EC 1935/2004 regulations. Optional certificates such as ATEX, 3.1 material certs, EAC, IECEx, UL are also available.
Our History
Antony Hare
Antony Hare has been part of Farleygreene since 1993, when he joined as a machine fitter on the factory floor. Today, as Managing Director, he leads a business that operates in nearly 30 countries and has been designing and manufacturing industrial sieving equipment for 50 years. The journey through every department in the company, through periods of significant change, and through the personal challenge of taking over a family business at short notice, has shaped both the leader and the company he runs.
A business founded on engineering principle
Farleygreene was founded in 1976 by Antony’s father, Alan Hare, and his business partner Peter Davies. Both were chief design engineers who set out to build sieving equipment to a higher standard than the market was offering at the time. The founding principle was straightforward: engineer it properly, build it to last and stand behind it. That principle has not changed in 50 years of operation.
Antony did not initially plan to join the family business. When he did, his father made a deliberate decision to start him on the factory floor as a machine fitter, learning the product from the inside out. It was not always comfortable at the time, but it proved formative.
“My father never gave me an easy ride. He wanted me to understand how everything worked – the machines, the people, the process. Looking back, that was a great gift: a deep experience which helps me understand how to serve our customers better.”
Antony worked his way through every department, from design, testing and manufacturing, to sales, before taking on a leadership role. This breadth of hands-on experience underpins how he runs the business today.
Evolving the manufacturing model
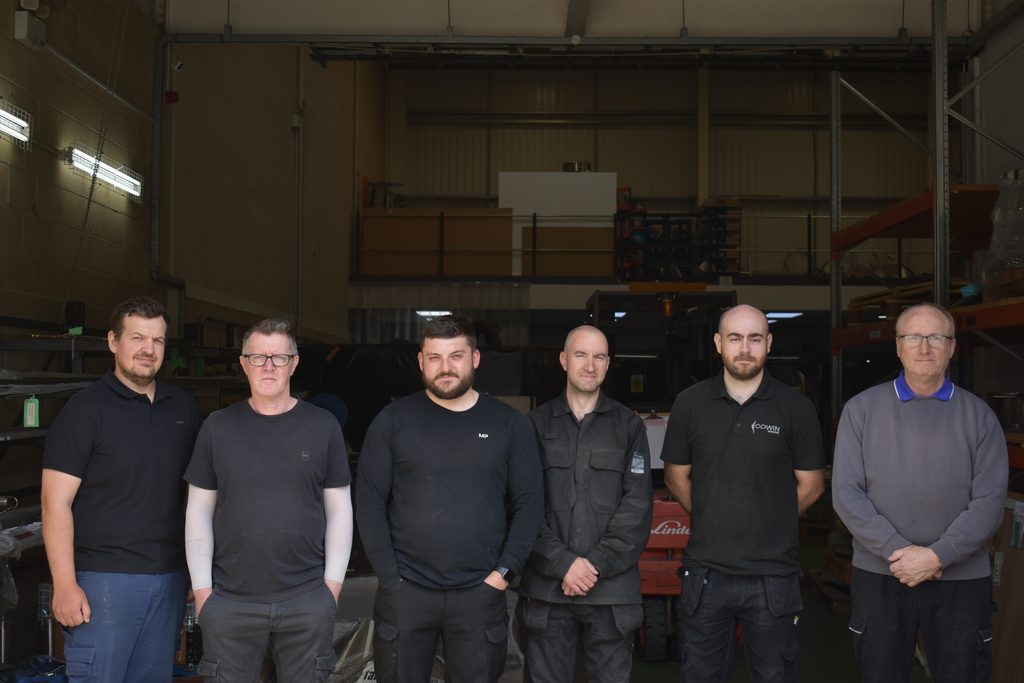
In the early 2000s, Farleygreene moved to a subcontracted component model, sourcing fabricated parts from trusted local UK suppliers and carrying out final assembly at their Hampshire facility. Two decades later, the decision was made to bring fabrication progressively back in-house, for greater control over quality, lead times and cost. Today the workshop team has grown to seven, with continued investment in new tooling (including an imminent laser cutter) and the expectation of reaching approximately 70% in-house production. All manufacturing remains UK-based.
“The move back to in-house fabrication is about quality and control as much as cost. When your manufacturing team is in the same building as your engineers, problems get solved faster, and the product gets better. That’s good for us and good for our customers.”
Stepping up – and raising the standard
The 2008 financial crisis had created an opening for smaller, more responsive suppliers, as customers who had previously worked exclusively with larger manufacturers began looking for alternatives. When Antony stepped up to lead the business following his father’s sudden death in March 2010, Farleygreene was well placed to capitalise on that shift.
The following year brought one of the company’s most significant commercial breakthroughs. A French OEM (which later became part of the Tetra Pak group) tasked an engineering intern to explore alternative sieving suppliers internationally. They found Farleygreene, requested a quote, and worked closely with the team to develop a solution that met their requirements precisely. The result was addition to a key approved supplier list, which in turn opened the door to relationships with major global food manufacturers including Nestlé and Danone, and to a significant increase in OEM business.
“That period taught us a lot. Larger customers with demanding specifications found that we could match or exceed what they were getting elsewhere – and we were easy to work with. We respond fast, we are flexible, and when something needs solving, we solve it. That reputation has stayed with us.”
The episode also reinforced the company’s commitment to high-specification manufacturing as standard. Where some suppliers offer upgraded materials such as 316 grade stainless steel (required for all food-contact components) as a premium option, Farleygreene’s baseline specification reflects what demanding customers actually need.
How Farleygreene works with customers today
The business today supplies sieving and screening equipment across food and drink, pharmaceutical, chemical, and additive manufacturing sectors. Orders range from standard configurations through to fully bespoke solutions designed for a specific application – some of which become the basis for new standard products. The engineering team’s experience across decades of applications means they can identify where a standard configuration needs adapting, and have the in-house capability to make those changes without compromising delivery or quality.
Every enquiry is supported by a material testing database built up over decades, allowing the team to predict how a specific product will behave on a given machine and advise accordingly. Customers frequently arrive with assumptions about their material (such as particle size, flow behaviour or bulk density) that testing reveals to be incomplete. Getting that right before the machine is specified saves considerable time and cost downstream.
“Customers often arrive with a specification based on what they think their product is. Our testing frequently reveals something different. Getting that right before the machine is built saves a lot of problems later.”
The engineering team works in SolidWorks, which has transformed both the design process and the customer experience. 3D models allow customers to visualise exactly how equipment will integrate into their production line before a machine is built, reducing installation surprises and speeding up internal approvals.
The six-step consultation process – from initial application request through to ongoing support – is designed to ensure nothing is assumed and nothing is missed. Farleygreene operates a structured follow-up process after every delivery to capture feedback and ensure the engineering team has visibility of real-world performance. When issues arise, they are tracked, addressed, and fed back into the product development process.
“When something goes wrong – as occasionally they do – the way we deal with it tells customers more about us than when everything runs smoothly. We take it seriously and work hard to be a company that’s there for customers for the long term, not just until the machine is installed.”
UK manufacturing, global reach
All Farleygreene equipment is designed and built in the UK, certified to ISO 9001, ATEX, CE, and UKCA standards, and supported by a global distributor network covering nearly 30 countries. For the large multinationals that now form a significant part of the customer base, UK manufacture and internationally recognised certification are precisely what their procurement standards require.
The company has also retained the scale and culture that allows it to work differently from larger competitors. Customer relationships are direct and long-standing – some customers have been with Farleygreene for decades. Decades of application experience mean the engineering team can identify where modifications are needed and make them in-house – without compromising on delivery or quality. The people making the decisions are the same people who built the product and know it in detail.
“We’ve spent 50 years earning the trust of some of the most demanding customers in the world,” confirms Antony. “In the sieving industry, experience and expertise are what that trust is built on – and we continue to demonstrate both.”
Find out more about Farleygreene
To learn more about Farleygreene’s history, products, and approach, visit the About Farleygreene page, explore the full sieving and screening product range, or contact the team to discuss your requirements.
About the author
Antony Hare is Managing Director of Farleygreene, a position he has held since 2010. He joined the company in 1993 and has worked across every department of the business. Connect with Antony on LinkedIn.
Luke Wilcox
Luke Wilcox joined Farleygreene ten years ago as a graduate design engineer. Since then, he has held almost every technical role in the business – design, certification, quality, and now manufacturing operations. That breadth of experience shapes how Farleygreene’s equipment is built, checked and delivered to customers with the most demanding process and hygiene requirements.
A career built across every technical discipline
Luke arrived at Farleygreene straight from his engineering degree and moved quickly into senior design work – developing both standard product designs and bespoke configurations for customers with specific process, hygiene or installation requirements. Feed inlet positions, frame mounting arrangements, cleaning access points: all of it designed from the outset to meet the hygiene standards demanded by food and pharmaceutical production.
From design, Luke moved into the technical and certification side of the business, taking responsibility for ISO 9001 compliance and QAN audits, ATEX certification, and the regulatory documentation that underpins every machine manufactured by Farleygreene. The role required him to demonstrate not just that individual products were safe, but that the company’s processes were too.
A period as Quality Manager followed: overseeing goods-in inspection, supplier management, customer complaints, and the technical files required for external certification of every machine as well as Farleygreene itself.
“Working across design, certification and quality has given me a really clear understanding of the high standards we must meet with every sieve machine we produce. It means I approach manufacturing with a constant drive to produce the best.”
Taking manufacturing in-house
Farleygreene sieving machines have always been manufactured in the UK, but until recently, Farleygreene relied on subcontractors for many components, with final assembly carried out on-site in Hampshire. Now, the team are bringing fabrication in-house, driven by growth, greater ability to control quality, and the need for faster turnaround. Today, Luke manages a team of five specialist welders, alongside inspection and an expanding range of on-site fabrication equipment.
As Luke confirms, the shift has been significant for customers as well as the business. With design and manufacturing under the same roof, the feedback loop between the engineering team and the workshop is immediate.
“Design queries get resolved in hours rather than days. Bespoke requirements can be prototyped, checked and refined without the delays that come with external suppliers. And costs passed on to customers are meaningfully lower.”
Why welding quality is key
Hygiene standards and the ability to keep machinery clean are critical in sectors such as food, pharmaceuticals, and chemical processing. Maintaining hygiene standards in sieving operations depends on much more than the design of the sieve: the quality of every weld on the finished product is crucial.
Farleygreene manufactures exclusively in 316 stainless steel, a premium alloy renowned for its superior durability and outstanding resistance to corrosion and the industry standard for hygienic applications. But the material choice is only part of the story.
Luke’s welding team works across MIG, TIG and laser welding processes, depending on the joint, the application, and the hygiene requirement – which extends beyond the generic standard of general fabrication.
“You can look at machines from other suppliers and see where the detail hasn’t been followed through. Welds that aren’t properly joined, surfaces that haven’t been finished correctly. Our guys take real pride in their work – tight seam welds, good fabrication, an eye for detail. It looks better, and more importantly it performs better in a hygienic environment.”
A fill-in weld used to compensate for poorly fitting components may appear to close a gap, but the resulting surface can lack the smooth, continuous finish required for effective hygiene and cleaning. In a food or pharmaceutical environment, that is not acceptable. Strength and durability can also be compromised if corners are cut in this advanced manufacturing sector. Luke’s team is trained to fit components accurately before welding, giving the highest level of protection and resilience.
The same high standard across every sector
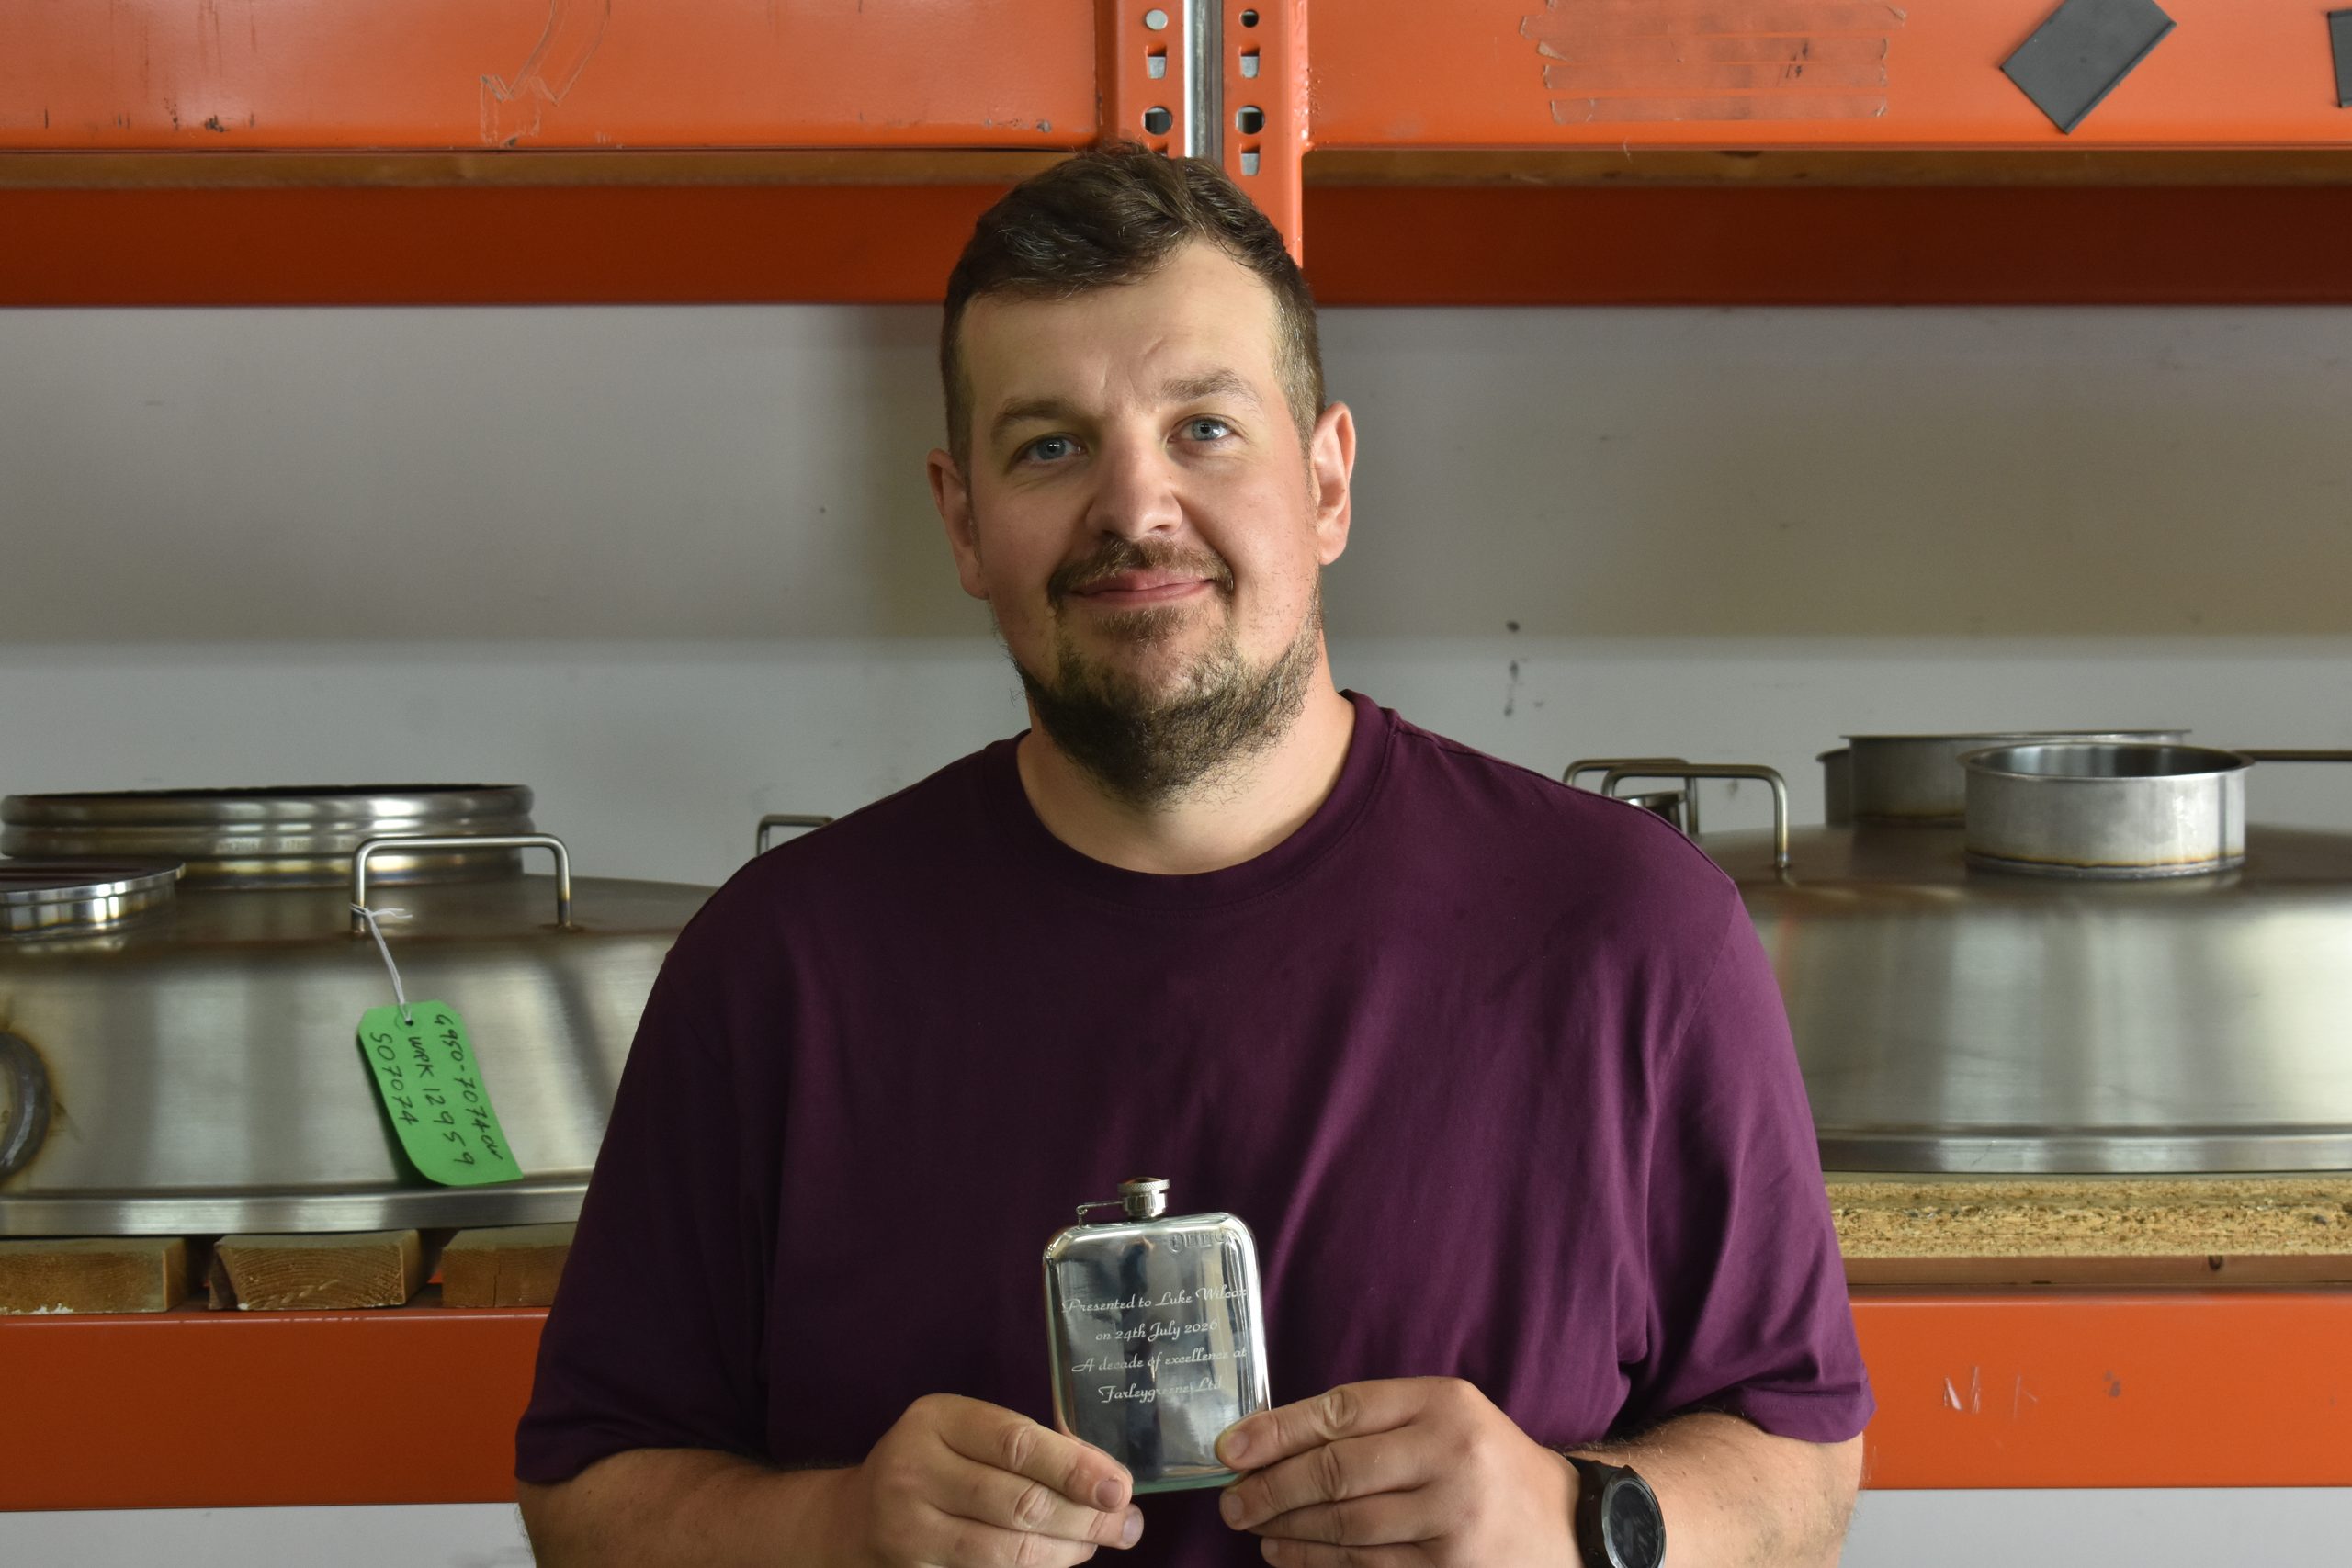
Farleygreene supplies sieving equipment across sectors including food and drink, pharmaceutical, chemical, and additive manufacturing. The manufacturing standard applied is consistent across all of them, because the hygiene and safety requirements of food and pharmaceutical production set the quality standard.
There are limited areas where customers can choose to specify differently. Surface finish options such as mechanical polish or beadblast, for example, may not be required for all applications and can represent a cost saving where hygiene standards permit it. But the underlying manufacturing quality of the weld integrity, the material specification, and the dimensional accuracy do not vary.
“We try to apply the same high standard whatever the sector. It’s easier to maintain quality consistently than to manage different standards for different customers. And it means every customer gets a machine that’s built properly, whatever their application.”
Continuous improvement as standard
Luke’s role spans not just day-to-day manufacturing operations but the ongoing development of Farleygreene’s production capability. New tooling is designed and built in-house where needed to achieve specific customer requirements.
The same engineering rigour that shapes the production process applies to the company’s certification and compliance work. ATEX certification, ISO 9001 accreditation, and the technical documentation required for international supply are all maintained and developed as the regulatory landscape evolves. All this is underpinned by the institutional knowledge Luke has built across every technical function in the business.
Speak to the Farleygreene team
To find out more about how Farleygreene’s equipment is designed and built, or to discuss a specific manufacturing or application requirement, contact us or connect with Luke on LinkedIn.
About the author
Luke Wilcox is Manufacturing Operations Manager at Farleygreene, with a decade of experience spanning design engineering, technical certification, quality management, and production. Connect with Luke on LinkedIn.

Rob Burnley
Rob Burnley started in purchasing administration at Farleygreene, but rapidly progressed through buying roles. Since 2018 he has been in aftersales, becoming Aftersales Manager in 2024, helping customers to get the most out of their Sievmaster and Sievgen industrial sieves.
Supporting customers after purchase
Farleygreene’s Aftersales department deals with spares, servicing, warranty claims, and what Rob terms ‘Level 1 technical support’ (basic troubleshooting). Spares and accessories available include the meshing of new and existing frames and rings, mesh rolls and panels (including woven mesh, perforated, wedge wire, and synthetic), replacement vibratory motors, magnets, rubber gaskets, earthing kits, toggle clamps, suspension mats, springs, and much more.
Typically, customers contact the department by email – usually in urgent need of a spare part that they may have mislaid or forgotten to order.
“Our customers know that specific parts on industrial sieves will need regular replacement, but if they are reluctant to keep them in stock, we do our best to help,” says Rob.
Indeed, Managing Director Antony Hare has recently invested heavily in maintaining stocks of critical consumables, knowing that customers face expensive downtime if they have not ordered their own spares in time. It is a conscious effort to provide further support to customers, says Rob: “We want to keep customer machines running smoothly, so we now go the extra mile to stock items such as gaskets and suspension mats, ready to ship.”
Some spares cannot be kept in stock at Farleygreene because there are so many variations. Mesh rings, for example, must be made to order to fit the customer’s specific machine and the material to be processed, with different sizes, mesh size and design. Here, the Aftersales team can quickly take an order, but the turnaround will be longer because the item must be made prior to dispatch.
A wide range of sieving models and spare parts
Every Farleygreene machine is designed and manufactured in house, so despite the wide range of products available, the Aftersales team can liaise with directly with expert engineers to understand exactly how your machine was built, and how it behaves in service. Often, customer issues turn out to be maintenance or configuration factors that are easy to fix.
“Ideally, a customer will give us the serial number of the machine, which can direct us straight to the right parts or requirements. Otherwise, we look at images and track parts using exploded diagrams; or we liaise directly with our on-site engineering team to ensure we can identify the problem and deliver the replacement part.”
Rob is still helping support customers with machines built in the early 1980s, drawing on a large paper archive to help find the right solution to get their industrial sieve back up and running.
“There’s no built-in obsolescence with a Farlygreene machine. We build products to last, so customers can trust our equipment. Of course we develop new sieving technology, but we are always happy to supply spares or even modify and upgrade older models.”
Worldwide aftersales and engineering support
Farleygreene sieves are found across the world, sold direct or through a wide network of trusted distributors. Aftersales for all these areas is covered by Rob and his team, with the support of engineers who will travel to site if necessary.
“Buying a Farleygreene sieve is a wise investment. We advise on the sieve and method that will work best for your material, we build the machine to order, and my team provides a strong and responsive aftersales service,” concludes Rob.
British manufacturing, built to last, with the support you can trust.
Read here to find out how to track down your machine’s serial number before contacting our Aftersales Department. Look for your Spares and Accessories here, or for more about aftersales and service from Farleygreene, contact us.
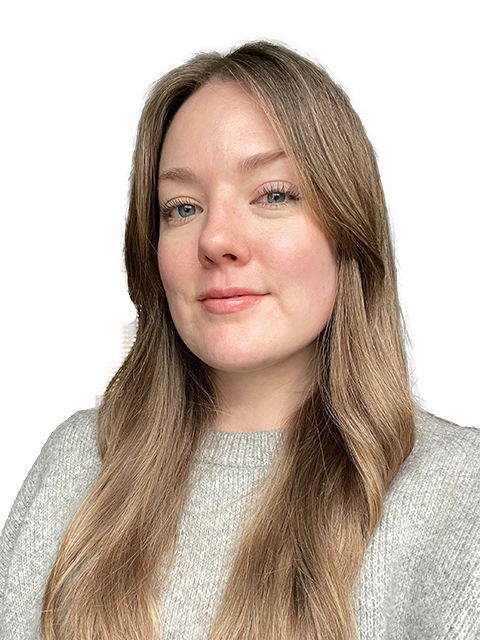
Charlotte Brooks
Charlotte leads Farleygreene’s marketing department, driving strategic marketing initiatives that support the company’s extensive portfolio of industrial and screening technology across global markets.
“We help our customers best when we understand what they need to sieve, their process and their specific challenges. It’s our job to share our cross-industry experience and sieving expertise, helping customers trust that Farleygreene has the knowledge and expertise to solve their sieving problems.”
Building relationships of trust
While technical performance is critical, purchasing decisions are often built on trust and confidence. Since joining Farleygreene in 2017, and subsequently becoming part of their Senior Leadership team, Charlotte has worked closely with the sales, engineering, aftersales and leadership teams to understand how to meet evolving customer needs. She believes this cross-functional perspective delivers valuable insight into the operational challenges customers face.
“After almost a decade in the business, I have developed a deep understanding of the industries we support, and the challenges faced by food, pharmaceutical, chemical and additive manufacturers around the world. This understanding informs Farleygreene’s strategy, and how our products and services should continue to evolve.”
Sharing the expertise of the Farleygreene team
“Customers increasingly want to know more about the expertise behind the equipment” says Charlotte. “They want insight into the people they are partnering with, evidence of how similar challenges have been solved, and confidence that support will continue long after installation.”
Farleygreene has over 50 years’ experience in solving real sieving problems across food, pharmaceutical, chemical, additive manufacturing and specialist processing industries. With a founding philosophy that the sieve must fit the material being sieved (not the other way round) the company delivers reliable sieving performance in any application, in any industry, by understanding the customer’s material, process and production environment first, then choosing equipment that fits all three.
This level of experience and expertise in industrial sieving is what Charlotte and her marketing team share with customers, giving them confidence that the sieving equipment designed and tested in house by Farleygreene will work with their material, in their process, under their real production conditions.
“Sharing this application knowledge, engineering expertise and real customer experiences is often just as valuable as sharing technical data, because it helps customers make informed decisions with confidence. While technical performance is critical, purchasing decisions are often built on trust, confidence and the reassurance that they are working with people who genuinely understand their challenges.”
New ways to reach and support customers
Farleygreene’s marketing activity has evolved significantly since Charlotte joined the company. What was once focussed largely on trade publications, exhibitions and website management has developed into a global, multi-channel programme encompassing digital advertising, technical content creation, video production, social media, search optimisation and, more recently, Generative Engine Optimisation (GEO) for AI search tools. Yet despite the channels changing, the objective remains the same: helping customers find reliable information that enables them to solve manufacturing challenges and make better decisions.
Charlotte knows that customers expect clear, accurate and authoritative information wherever they choose to search. For specialist engineering manufacturers like Farleygreene, success increasingly depends on demonstrating genuine expertise through practical guidance, educational resources and real-world application knowledge.
“I am particularly interested in understanding why people make decisions and how businesses can communicate more effectively. Every day, I ask myself ‘Why are we doing this? What problem are we solving? How does this help our customers?’ – ensuring that every marketing initiative remains focused on delivering genuine value to customers.
Commitment to solving customer sieving problems
Charlotte is confident that Farleygreene will continue to strengthen its position as a trusted global specialist in sieving and screening technology, while expanding its reach into new industries, applications and markets.
“While marketing technologies and communication channels will continue to evolve, our commitment to engineering excellence, customer focus and helping manufacturers solve real-world processing challenges will remain at the heart of everything we do.”
To find out more about why you can trust Farleygreene’s expertise, contact us or connect direct with Charlotte on LinkedIn.
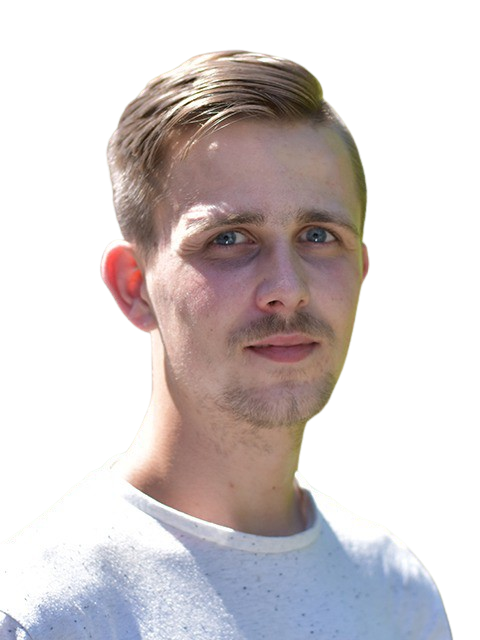
Gareth Gallagher
Gareth’s role as Production Control Manager means his work has a direct impact on customers. Through effective capacity planning, scheduling and workflow controls, he can give customers realistic delivery times for their specific sieving machines, and honest updates if any issues arise.
“At Farleygreene, quality trumps everything else. All our industrial sieves are bespoke, so I can track the progress of each one and make sure they meet the required standards before they leave our premises.”
Experienced in manufacturing and product assembly
Gareth had several years of practical engineering experience before joining Farleygreene in 2018 as a Production Engineer. Since 2024 he has been Production Manager, in charge of each order from the time it is handed over by the administrative and engineering teams right through to delivery.
This familiarity with how the products are manufactured means that Gareth is equally comfortable checking progress on the shop floor, liaising with any external subcontractors and double-checking lead times with Farleygreene’s engineers.
“Our manufacturing software provides good time estimates, but since much of the detailed work is bespoke, I need to make sure that both our in-house fabricators and subcontractors will have everything they need to meet on-time delivery.”
Real-time updates, direct from the shop floor
Like most of the Farleygreene team, Gareth works on site, so he can easily ask engineers to check details, or verify that sieving products are on target. With a move to more in-house fabrication, this collaboration has become even more versatile. Gareth’s hands-on approach means customers frequently give great feedback on Farleygreene’s customer service.
“Customers tell me they really appreciate how easily they can get in touch: unlike in larger organisations, I know their product and can give them real-time progress updates, even sharing images of their sieve in production or before dispatch.”
Care from order to delivery
Once customers have discussed the options with Farleygreene’s engineers and sales team, their sieve is designed to order. The bill of materials is issued, engineering drawings pulled, and Gareth and his team schedule the workflow, keeping the customer updated right through to delivery.
At every stage, Gareth is responsible for checking the teams have what they need, including ensuring that any subcontractors have clear instructions and specifications.
“Our working environment is very collaborative, and recent internal restructuring to ensure colleagues can work in areas that interest them has given me more time to visit and check on our subcontractors too, helping to ensure we deliver to exacting standards across the board.”
Once assembly is complete, every sieve machine goes through checks by the assembly team, with a repeat check by Gareth or another colleague, and then undergoes any Factory Acceptance checks required by the customer.
“Our customer service and quality standards define Farleygreene’s offer,” says Gareth. “The team are passionate about only sending out products that are built properly, and as a personal principle I am always open with customers, even on the rare occasions when something is delayed. It’s a two-way street, everyone benefits, and we keep our reputation for high quality industrial sieves with great customer service.”
To find out more about how Farleygreene keeps every bespoke order on track from design to delivery, connect with Gareth on LinkedIn.
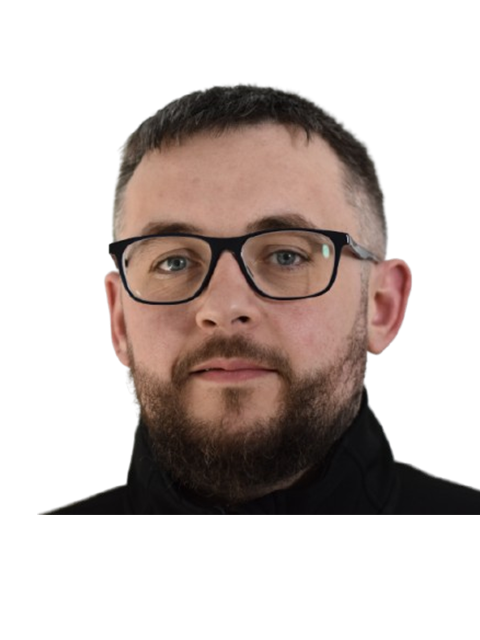
Phil McFarland
As Senior Buyer, Phil McFarland is responsible for sourcing the materials and components that go into every Sievmaster machine.
“All Farleygreene products are built to high quality standards, which means that high quality procurement and stock management are essential. My team works hard to ensure a strong supply chain with exacting standards, so that customers secure the best quality sieving machines.”
Sourcing without compromising on quality
Farleygreene fabricates much of its own equipment in-house, so Phil’s team sources incoming raw materials, components and some external fabrication services. Supplier quality control remains a core part of the role, as the quality of incoming material feeds directly into the quality of the finished component.
Phil’s job involves screening potential suppliers (many of whom fail the quality test), with front end verification and onboarding followed by ongoing QA checks to confirm they remain suitable. If issues arise, he deals with audits and reviews, managing the process to ensure that Farleygreene’s exacting standards are met.
Supporting the move to in-house manufacturing
From a purchasing perspective, the shift toward in-house manufacturing has meant buying in more raw materials and moving fabrication onsite, keeping quality control closer to home. Any issue the QA inspector identifies can now be addressed with the workshop team directly, rather than routed back through an external supplier.
Because Farleygreene sells to order rather than working from long-term supply contracts, inventory management is a significant part of the role: holding enough stock to meet demand without overstocking, and making sure the data on the system reflects what is actually on the shelves. Phil’s department has also recently taken on responsibility for the shipping function at Farleygreene, further expanding his expertise within the supply chain.
Experience in procurement
Before joining Farleygreene, Phil spent three years in distribution for a book publishing company, which piqued his interest in purchasing. Looking for a new role in procurement, he joined Farleygreene in 2021 as a purchasing administrator and within six months had been promoted to Senior Buyer by Managing Director Antony Hare.
As a result, Phil has worked from the ground up to learn about procurement, including achieving a Level 4 CIPS (Chartered Institute of Procurement & Supply) Diploma in Procurement and Supply Chain Management. He has built a set of standard operating procedures for the department to keep processes consistent and fit for purpose as the team grows, and shares what he has learned with the people he manages.
Ambitious and results-driven, Phil is always keen to learn more and to share best practice with his team, so that Farleygreene customers ultimately benefit from the best quality products at the best price.
Leading with trust and respect
Phil’s approach to managing his team centres on treating people, suppliers and colleagues alike, with trust and respect. He wants his work and his team to reflect the values he sees instilled at Farleygreene: taking pride in building high quality products, and being seen as people who are good partners in business.
“Negotiating, sourcing and protecting quality all work best when you treat people the right way, whether they aresuppliers or colleagues. I am proud to be part of the Farleygreene family, ultimately making sure that we always bring the best to our customers.”
Find out more about Farleygreene
Learn more about Farleygreene’s expertise in British Engineering, or explore our sieving product range. Please get in touch if you have any questions, we’re happy to help.
Join Farleygreene
Here at Farleygreene we are a family owned company that expects the team to deliver and develop day after day, just like our customers do.
We aren’t currently recruiting at this time, but please get in touch if you feel you have something to offer.
Get in touch to work with us
We are actively looking to increase our reach around the world so if you feel you have something to offer as a potential employee, distributor, or supplier then please get in contact with us.